Advanced Thermal Recycling (ATR®) Technology Explained
Advanced Thermal Recycling Technology
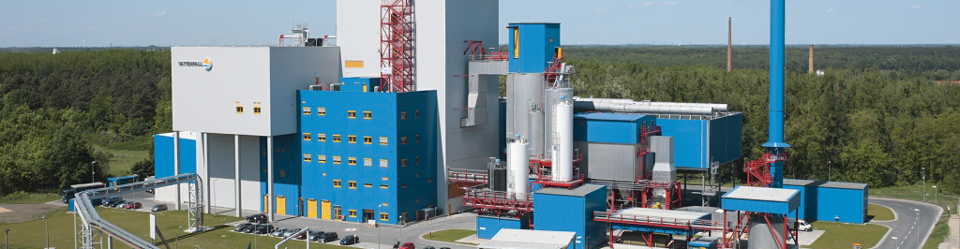
Advanced Thermal Recycling (ATR®) resets the standard for MSW conversion technology by combining the lowest achievable emissions with the highest landfill diversion rate of any commercially-available technology.
What the Plant Is Built From
The solid waste combustion system, boiler, combustion control system and air pollution control equipment are supplied by Fisia Babcock Environment GmbH (FBE), which has installed 470 commercial-scale solid waste combustion units over the last 50 years and nearly twice that number of air pollution control systems. To that are added bottom ash and fly ash treatment systems that produce commercially reusable products, plus an optional pre-processing system to recover recyclable materials in the Municipal Solid Waste (MSW) delivered to the facility.
The ATR® Process
Overhead refuse cranes mix the waste in the bunker to create a homogeneous mixture, which matters for good combustion and low carbon content in the bottom ash by-product. A crane then feeds the mixed waste into the feeding hopper and down onto forward feeding grates. Each production line feeds a boiler housing a furnace operating above 1560°F for 2 seconds, with the temperature at the end of the combustion zone measured through acoustic monitoring. A computerized control system monitors temperature, grate speed and air volume so that complete combustion occurs; maintaining the furnace's high temperature is essential to rid the waste and the combustion gases of complex organic compounds such as dioxins and furans.
Flue Gas Treatment
Flue gas cleaning begins in the boilers, where oxides of nitrogen are reduced by injecting ammonia water into the combustion chamber using the SNCR method. Fly ash is separated downstream of the super heaters to prevent pollutant reformulation in the critical 600°F to 400°F range, and activated carbon absorbents injected after the first bag house capture reformed organics, condensed heavy metals and salts. Acid gases pass through a two-stage scrubber, then a counter flow neutral scrubber using lime slurry to remove sulphur oxides. A second bag house polishes out remaining aerosols, organics and heavy metals to levels usually below detection.
Energy and Marketable By-Products
Heat released in the boiler produces high pressure, super-heated steam, which generates electrical energy through a turbine-generator fed into the public power grid. Bottom ash is screened, crushed, freed of unburned material and washed for use as construction aggregate. Iron scrap and non-ferrous metals such as aluminum, copper and brass are separated for steel and metals production. Gypsum is sold to the construction industry, while acid scrubbing yields commercial grade 30% hydrochloric acid. Fly ash, up to 5% by weight of the MSW combusted, is treated to recover cadmium, copper, nickel, zinc and lead, taking overall ATR® landfill diversion to about 99%.
Learn More:
Specify an ATR® Facility for Your Waste Stream
Klean Power engineers Advanced Thermal Recycling facilities around FBE combustion and air pollution control equipment, bottom ash and fly ash treatment, and optional MRF pre-processing.
The proven performance of the ATR® processes represents the yardstick against which all MSW conversion technologies are to be measured, with an overall landfill diversion rate of about 99%.
What tonnage and waste composition are you planning around?
Contact Klean Industries about Advanced Thermal Recycling technology » GO.